
Automotive Parts Painting Line for Fasteners & Small Parts: High Volume, Low Cost
Fasteners and small stamped parts are the unsung heroes of automotive assembly. They are produced in millions, cost pennies each, and yet must meet strict corrosion and torque specifications. The painting line for these parts must achieve one thing above all: the lowest possible cost per piece while maintaining consistent quality.
Typical Parts We Paint
- Bolts and screws (M6–M20)
- Washers and spring washers
- Clips, pins, and retaining rings
- Springs (coil, leaf)
- Small stamped brackets
- Nuts and inserts
Recommended Process: Powder Coating / Batch Oven Systems
Process Option A: Electrostatic Spray + Conveyorized Oven
Best for medium-sized parts (50–500 g each) with moderate volume (100,000–1,000,000 pcs/month).
| Parameter | Value |
|---|---|
| Application | Automatic electrostatic spray guns |
| Conveyor | Overhead monorail with custom racking |
| Cure | Gas or electric conveyor oven, 180–200°C |
| Throughput | 500–5,000 pcs/hr depending on rack density |
Process Option B: Fluidized Bed Dip Coating
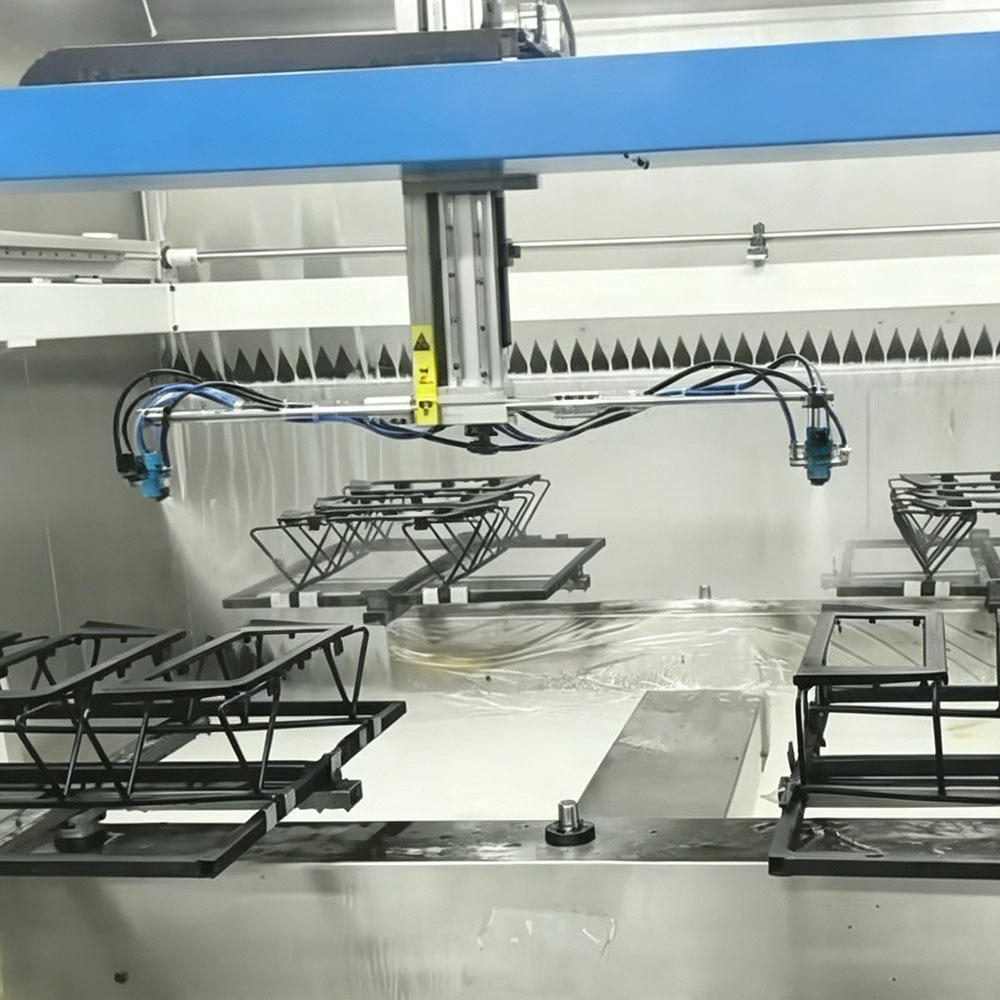
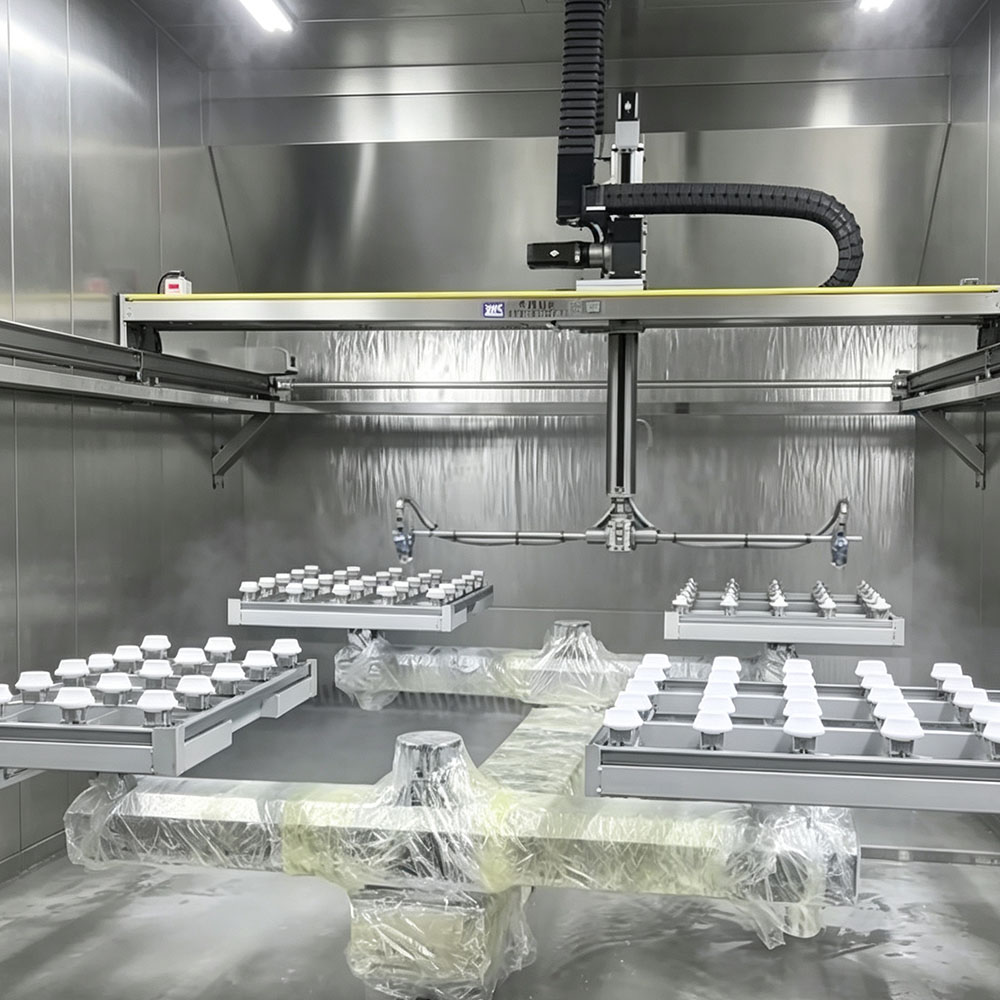
Ideal for small, dense parts that are difficult to spray evenly. The part is preheated, dipped into a fluidized bed of powder, and the heat melts the powder into a uniform coating.
 |  |
| Parameter | Value |
|---|---|
| Application | Fluidized bed dip |
| Film Thickness | 100–300 µm (thicker than spray) |
| Cure | Post-heat in batch oven |
| Best For | Bolts, clips, irregular small parts |
Process Option C: Batch Oven System
For low-mix, high-volume production. Parts are loaded into racks or baskets, sprayed or dipped, then cured in a box oven. Lower CAPEX, flexible batch sizes.
Key Buyer Concerns — Answered
1. Racking Density Optimization
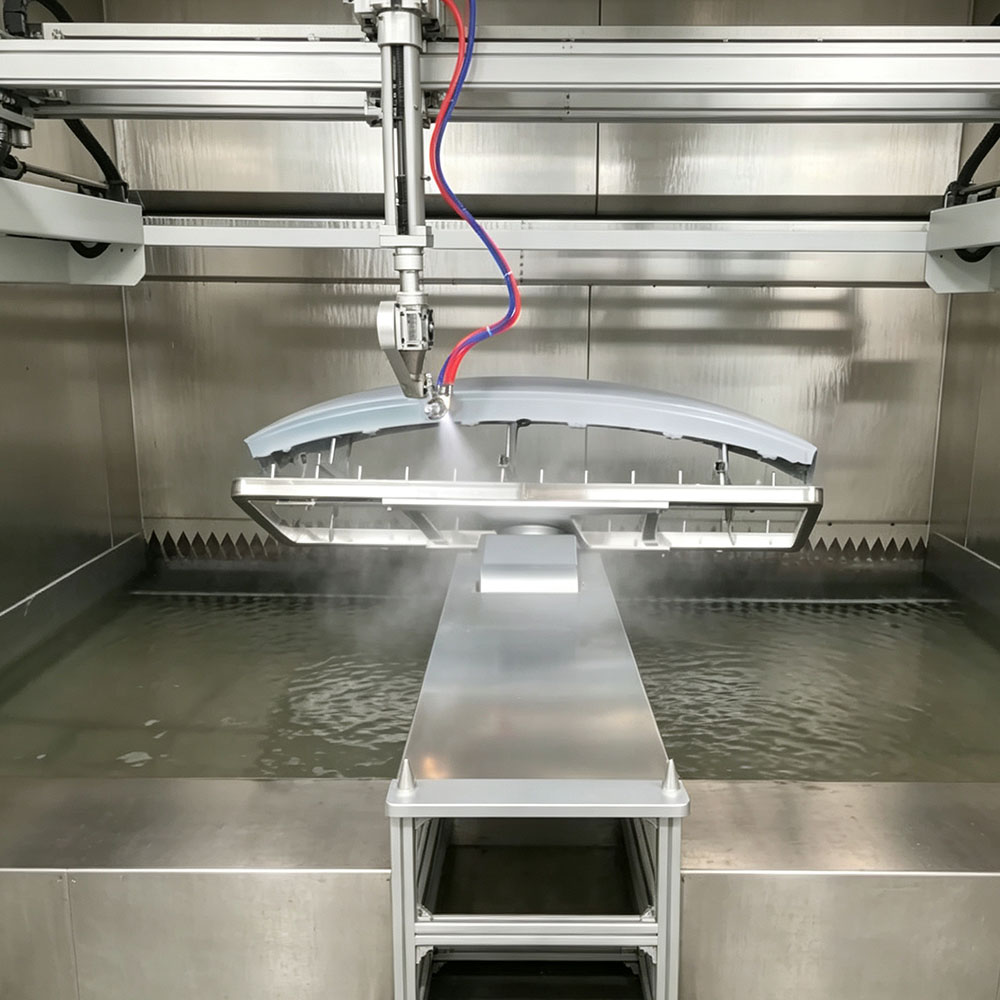
The single biggest factor in per-piece cost is how many parts fit on a rack. Our engineers design custom racking solutions that maximize density while ensuring proper grounding for electrostatic adhesion. A well-designed rack can double throughput without increasing line speed.
2. Powder Transfer Efficiency
Small parts create challenges for powder wrap and Faraday cage effects (in recesses and threads). We use corona-charge guns with adjustable kV and amperage, plus tribo guns for recessed areas, achieving >85% first-pass transfer efficiency.
3. Automation: Vibratory Screening & Auto-Recovery
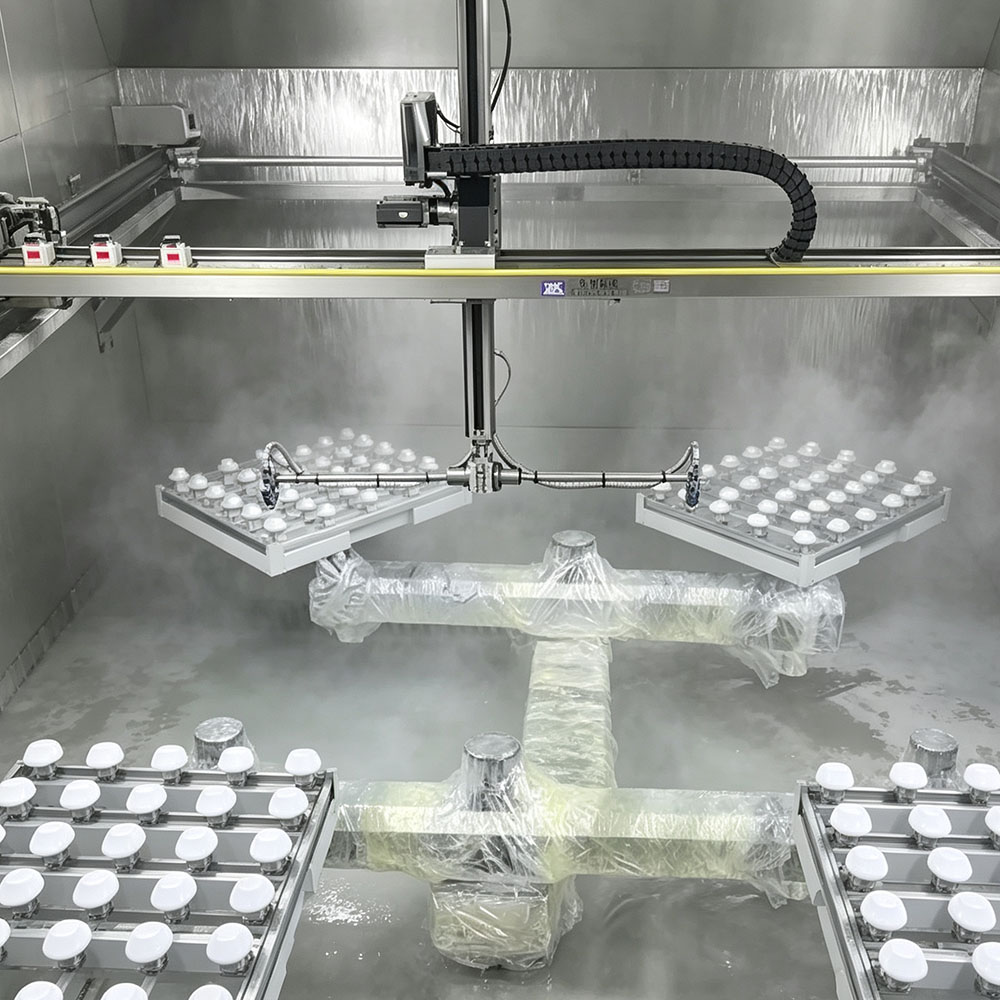
To keep labor costs down, our systems include automatic powder recovery, vibratory sieving to remove contaminants, and PLC-controlled gun triggering that only sprays when parts are present—reducing overspray waste to near zero.
 |  |
Cost Comparison (per 1,000 parts)
| Method | Material Cost | Labor Cost | Total Est. |
|---|---|---|---|
| Electrostatic Spray + Conveyor | $3–5 | $2–3 | $5–8 |
| Fluidized Bed | $4–6 | $1–2 | $5–8 |
| Batch Oven (manual) | $3–5 | $4–6 | $7–11 |
Geetech Advantage
We have delivered small-parts painting lines to fastener manufacturers in China, India, and Turkey. Our modular designs allow you to start with a basic batch system and upgrade to a fully automated line as volume grows.
Cut Your Small-Parts Painting Cost
Send us a sample batch of your parts. We will coat them in our 4,000 m² testing workshop and report back with film thickness, adhesion, and per-piece cost data.
📞 WhatsApp: +86 135 9019 9492 | 📧 sales@geetech.co | 🌐 geetech.co